WhatsApp: +86 16626708626
 Email:
 Phone: +86 16626708626
Description
Key Technical Specifications
| Parameter | Specification |
| Part Number | A06B-0238-B605 |
| Manufacturer | FANUC |
| Model Code | \alpha iS 12/4000 |
| Rated Output Power | 2.7 kW |
| Maximum Speed | 4000 RPM |
| Stall Torque | 12 Nm |
| Shaft Specification | Tapered Shaft (TPR) |
| Brake Specification | Integrated 90V DC Holding Brake |
| Feedback / Encoder | \alpha 64iA High-Resolution Absolute Encoder |
| Input Voltage | 168V to 240V AC (Drive Dependent) |
| Cooling Method | Natural Convection / Flange Dissipation |
| Protection Rating | IP65 (Standard oil seal configurations) |
| Approximate Weight | 15.88 kg (35 lbs) |
Product Introduction & Supply Chain Strategy
The FANUC A06B-0238-B605 is an \alpha iS series AC servo motor designed to provide exceptional dynamic response, torque density, and precise feedback control for demanding CNC machining applications. Featuring a tapered shaft output, an integrated 90V DC mechanical holding brake for vertical/inclined axis safety, and an advanced \alpha 64iA optical encoder, this motor ensures micro-meter level positioning accuracy across milling, turning, and multi-axis machining centers.
When sourcing the A06B-0238-B605 for critical production equipment, acquiring tested units with verified encoder performance and coil resistance is crucial to maintaining machine calibration. Servomotor failure on an active production line leads to immediate axis faults (e.g., SV0401, SV0414) and costly unplanned downtime. Utilizing direct replacement units ensures seamless plug-and-play mechanical fitment and drive parameter alignment, reducing Mean Time to Repair (MTTR) while avoiding the risks associated with non-OEM motor retrofits.
Installation & Troubleshooting Guide
Stage 1: Pre-Installation (Safety & Preparation)
- Power Isolation: Lock out and tag out (LOTO) main power to the CNC cabinet and servo amplifier drive.
- Axis Securing: If replacing the motor on a vertical or angled axis, mechanically block or pin the machine head to prevent gravitational drop when the motor brake is released.
- ESD Safety: Wear grounded static protection when connecting the high-resolution feedback encoder cable.
Stage 2: Mechanical & Electrical Removal
- Unplug the motor power feedback connectors and the 90V DC brake release line.
- Loosen and remove mounting flange bolts; uncouple the tapered shaft from the axis gearbox or ball screw assembly.
- Inspect keyway/taper surfaces and mounting faces for burrs, debris, or oil ingress.
Stage 3: Installation & Alignment
- Align the tapered shaft with the machine coupling, seating the flange flush against the mounting surface.
- Torque mounting bolts evenly in a cross pattern to manufacturer specifications.
- Connect power leads, encoder harness, and brake lines, ensuring IP65 seals and cable strain reliefs are fully engaged.
Stage 4: Testing & Verification
- Re-apply power to the servo drive and clear any remaining axis fault codes on the CNC control.
- Verify 90V DC signal operation on the brake release during axis enable.
- Perform a low-speed jog test to verify rotation direction, encoder feedback counts, and quiet mechanical operation.
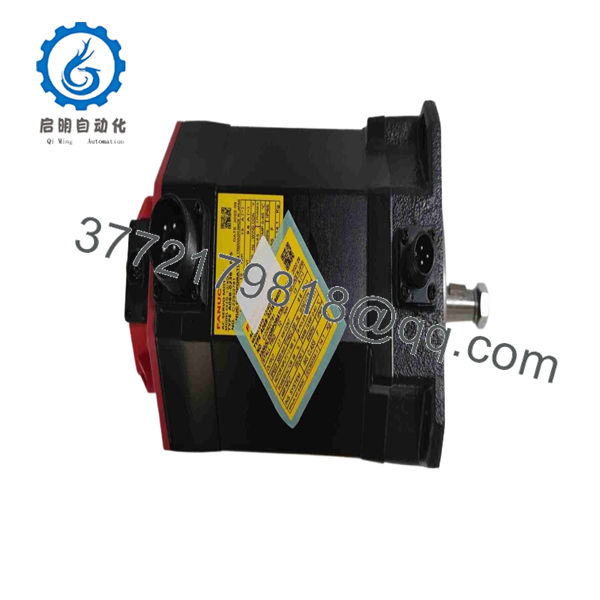
A06B-0238-B605
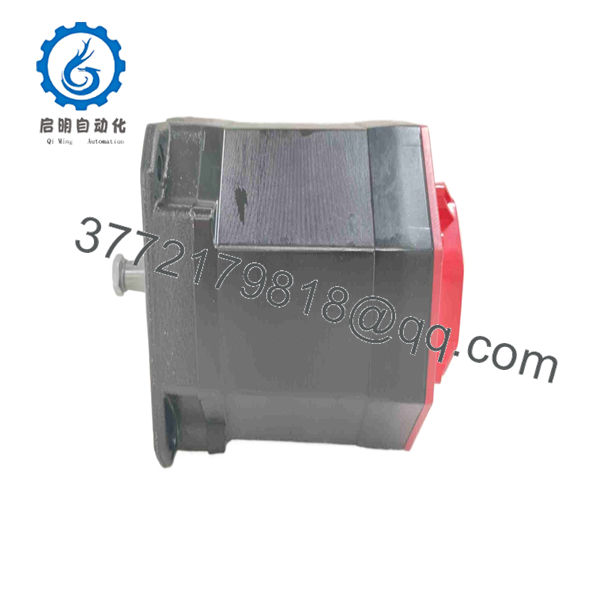
A06B-0238-B605
Drive Compatibility & Setup Notes
- Amplifier Matching: Compatible with FANUC \alpha i series Servo Amplifiers (e.g., A06B-6114 or A06B-6117 series drives).
- Encoder Calibration: Replacing the motor with an \alpha 64iA absolute encoder requires re-establishing the machine grid reference point (zero point/home position) via CNC parameter setting (e.g., Parameter 1815 for FANUC 0i/30i controls).
- Brake Power Source: Ensure the 90V DC supply circuit is protected with appropriate surge suppression to prevent voltage spikes from damaging the internal brake coil during quick-stop disengagements.
Frequently Asked Questions (FAQ)
Q: What shaft configuration does the A06B-0238-B605 feature?
A: This model features a tapered shaft (TPR) designed for high-rigidity force transmission in precision CNC machine couplings.
Q: Is the holding brake on this motor designed for dynamic stopping?
A: No, the 90V DC integrated brake is a static holding brake designed to keep vertical or inclined axes fixed when power is removed. It should not be used as a dynamic friction brake except during emergency stop conditions.
Q: Do I need to reset absolute position origin after installation?
A: Yes. Because the motor contains an absolute encoder (\alpha 64iA), replacing the unit requires resetting the reference position (zero point) in the CNC controller parameters.
Q: What is the primary difference between the A06B-0238-B605 and straight-shaft variants?
A: The -B605 suffix designates specific mechanical options, including a tapered shaft and an integrated 90V DC brake, whereas other sub-models may feature straight keyed shafts or lack holding brakes.