WhatsApp: +86 16626708626
 Email:
 Phone: +86 16626708626
Description
Key Technical Specifications
| Parameter | Specification |
| Manufacturer | FANUC Corporation |
| Part Number | A860-2109-T302 |
| Product Line | Alpha i Pulse Coder (aA1000i / aA1000iS Series) |
| Feedback Type | Optical Absolute Encoder |
| Resolution | 1,000,000 pulses/revolution (1,000k high-resolution absolute) |
| Interface Type | High-Speed Serial Communication |
| Motor Compatibility | FANUC Alpha i and Beta i Series AC Servo Motors |
| Connection Style | Multi-pin Circular Connector / Internal Ribbon Harness |
| Operating Temperature | −10 to +80 °C |
| Protection Rating | IP65 (when correctly sealed within motor housing) |
| Weight | Approx. 0.30 kg (0.66 lbs) |
Product Introduction & Supply Chain Strategy
The FANUC A860-2109-T302 is an absolute optical pulse coder engineered for precise rotor position sensing on FANUC Alpha i and Beta i series AC servo motors. Mounted directly on the rear shaft of the servo motor, this high-resolution feedback sensor translates rotary motion into high-speed digital serial data sent straight to the servo amplifier. It is essential for sub-micron positioning accuracy, smooth low-speed torque control, and maintaining absolute machine zero points without requiring manual homing cycles upon power-up.
From a supply chain perspective, stocking this encoder as New Surplus provides a direct shield against multi-day CNC machine stoppages. Refurbished encoders often suffer from micro-scratched optical glass disks, degraded LED emitters, and heat-stressed internal processing ICs that result in intermittent pulse counts, axis tracking errors, or thermal drift alarms under heavy machining loads. Purchasing New Surplus guarantees factory-fresh optical elements, uncompromised signal processing, and long operational life, minimizing Total Cost of Ownership (TCO) by keeping your primary CNC spindles and feed axes running reliably.
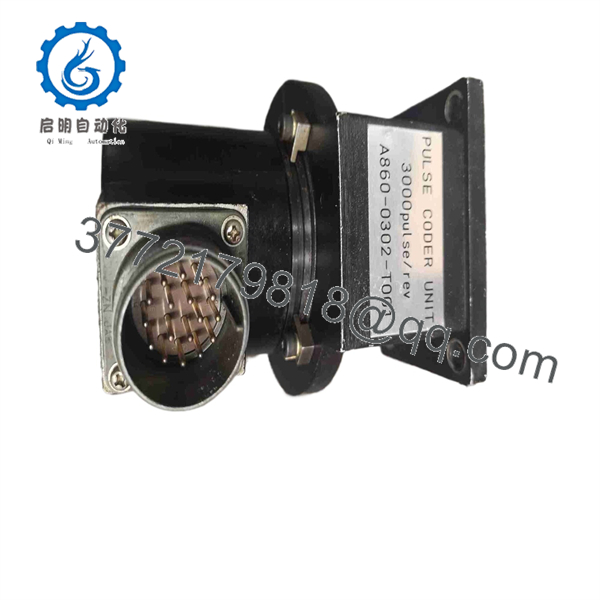
A860-2109-T302
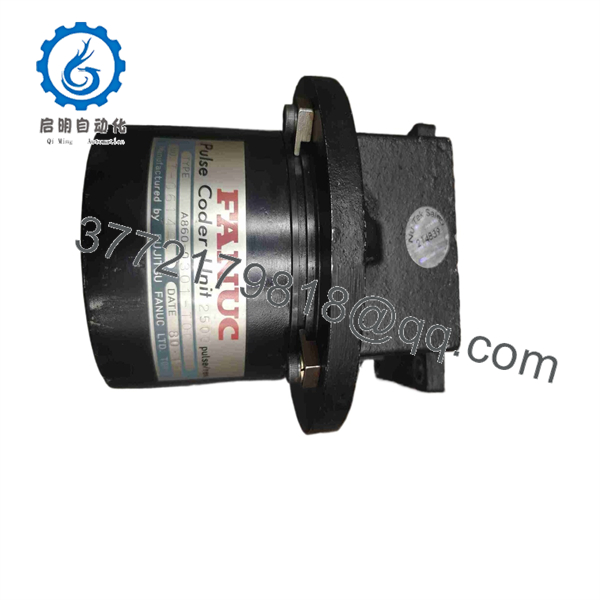
A860-2109-T302
Installation & Configuration Guide
1.Stage 1: Pre-Installation (Prep & Safety):Perform LOTO and protect encoder against ESD.
Disconnect main 3-phase power to the CNC machine enclosure and lock out the breaker. Allow all servo drive bus capacitors to fully discharge for 10 minutes. Wear a grounded ESD wrist strap before handling the rear motor end-bell or touching encoder wiring. Clean the exterior of the motor rear casing to ensure no coolant, oil, or metal filings drop into the optical cavity during the swap. Photograph all internal cable routing and mounting orientation.
2.Stage 2: Removal:Remove rear motor cap and detach old pulse coder.
Unbolt the protective rear motor cover. Unclip the multi-pin internal wiring harness connected to the pulse coder PCB. Carefully unscrew the encoder retaining bolts or mounting clamps. Pull the old A860-2109-T302 straight off the motor shaft end, ensuring you do not twist or force the delicate coupling or center alignment pin.
3.Stage 3: Installation (Clone & Seat):Align shaft coupling and torque fasteners evenly.
Inspect the motor shaft end for burrs, grease, or debris. Carefully line up the keyway or flexible coupling of the new A860-2109-T302 pulse coder with the motor shaft extension. Slide the unit evenly onto the shaft without hammering or applying axial impact. Tighten the mounting screws to specification in a star pattern. Reconnect the internal signal harness until the locking tab clicks into place, and reinstall the rear motor seal and cover.
4.Stage 4: Power-On & Testing:Power up drive, clear pulse coder alarms, and set grid zero.
Restore logic power to the CNC controller and observe the servo drive display. Clear any initial disconnect alarms (e.g., FANUC Alarm 350, 351, or 368) by cycling control power or performing a parameter pulse coder initialization. Perform axis homing or reset parameter 1815 (APZ) to establish the absolute machine reference zero position. Run the axis at low speeds in JOG mode to confirm smooth feedback tracking and zero position error drift.
Firmware/Software Versions & Upgrade Notes
- System Parameter Synchronization: The A860-2109-T302 communicates over FANUC high-speed serial bus protocol. The CNC control must have its servo parameters configured for the correct encoder resolution (e.g., setting the proper flexible feed gear ratios and pulse coder type parameters in the 2000 series parameter group).
- Hardware Suffix & Resolution Matching: Ensure you do not substitute this unit with incremental variants or different resolution suffixes (such as T201 or T301) without adjusting the CNC control’s internal servo parameter tables. An incorrect encoder resolution causes massive positioning errors and drive runaway alarms.
- Mechanical Handling Warning: The internal glass disk on the A860-2109-T302 is extremely sensitive to physical shock. Never strike the encoder body or motor shaft with a hammer during installation, as micro-fractures on the optical disk will permanently ruin feedback accuracy.
Frequently Asked Questions (FAQ)
Q: Why is this unit priced higher than refurbished options online, but lower than direct OEM list price?
A: This product is a Brand New Surplus unit. It is not used, not pulled from a decommissioned plant, and not refurbished. All modules undergo rigorous quality verification to ensure OEM-level reliability. Refurbished encoders often harbor hidden optical disk contamination and degraded light sources that lead to random axis alarms. Our pricing reflects genuine, factory-fresh global inventory offered at a lower cost than direct OEM list prices.
Q: Is the FANUC encoder still actively used, and why keep it in spare stock?
A: Yes, millions of FANUC Alpha i and Beta i motors equipped with this encoder drive production machines globally. Because a failed encoder immediately halts the affected axis and triggers drive fault alarms, keeping 1 to 2 units in safety stock prevents long machine downtime waiting for emergency replacement hardware.
Q: Will swapping this encoder require resetting the machine zero point (reference point)?
A: Yes. Because this is an absolute encoder, removing it from the motor shaft disrupts the mechanical coupling position. After installing the new , you must calibrate the absolute reference position (grid zero) on the CNC screen via parameter 1815.
Q: Can I hot-swap this encoder while the servo amplifier is powered on?
A: No. Disconnecting or plugging in the encoder signal harness while 24V logic power or main drive power is present will cause voltage spikes that destroy the delicate optical receiver ICs inside the encoder and on the servo amplifier control board. Always de-energize the cabinet first.
Q: What documentation and warranty coverage come with this pulse coder?
A: Every FANUC pulse coder is shipped in anti-static ESD packaging with verifiable OEM serial numbers and an accompanying QC inspection report verifying signal output integrity. We back this New Surplus unit with a comprehensive 1-year replacement warranty.