WhatsApp: +86 16626708626
 Email:
 Phone: +86 16626708626
Description
3. Key Technical Specifications
| Parameter | Value |
|---|---|
| Rated Output | 5.5 kW |
| Stall Torque | 30 Nm |
| Rated Speed | 3000 RPM |
| Maximum Speed | 4000 RPM |
| Voltage | 177 V |
| Rated Current | 19 A |
| Stall Current | 31.7 A (rms) |
| Shaft Type | Tapered (TPR) |
| Brake | 90 V BRK |
| Encoder | a64ia (Alpha i absolute) |
| Protection Class | IP65 |
| Insulation Class | F |
| Phases | 3 |
| Rotor Inertia (with brake) | Approx. 0.00819 kg·m² |
| Weight (with brake) | Approx. 29–31 kg |
4. Product Introduction
The FANUC A06B-0268-B605 is an Alpha iS series AC servo motor (model AiS30/4000) built for CNC machine tool feed axes. It delivers 5.5 kW continuous output with 30 Nm stall torque and a 4000 RPM maximum speed. The unit includes a tapered shaft and 90 V holding brake, paired with an a64ia absolute encoder.
This motor fits large machining centers and similar high-duty applications where consistent torque response and encoder feedback matter. Buyers choose it as a direct drop-in for matching Alpha iS systems when the original motor fails or needs upgrade. Verify exact amplifier pairing and parameter settings against the FANUC manual before installation.
5. Troubleshooting Quick Reference
| Symptom | Possible Cause | Relevance to this Part | Quick Check Method | Recommendation |
|---|---|---|---|---|
| No rotation, no current draw | Power or amplifier fault | ❌ Low | Measure 200–240 V AC at amplifier input; check DC bus | Check amplifier and fuses first |
| Motor hums but does not turn | Brake not releasing | ✅ High | Measure 90 V DC at brake terminals when enabled | Verify brake power supply and wiring |
| Excessive vibration or noise | Bearing wear or mechanical bind | ✅ Medium | Hand-rotate shaft (power off, brake released); listen for roughness | Replace motor if roughness present |
| Following error / position lag | Encoder feedback loss | ✅ High | Check encoder connector seating and cable continuity | Swap encoder cable; test motor on known-good amp |
| Overheat alarm after short run | Overload or cooling issue | ✅ Medium | Monitor load current vs. continuous rating; check ambient temp | Reduce duty cycle or verify mechanical load |
| Alarm on power-up only | Parameter or ID mismatch | ❌ Low | Compare motor ID in CNC parameters with nameplate | Confirm parameter set matches AiS30/4000 |
If the issue persists after these checks, send photos of the nameplate, diagnostic screens, and wiring connections for further support.
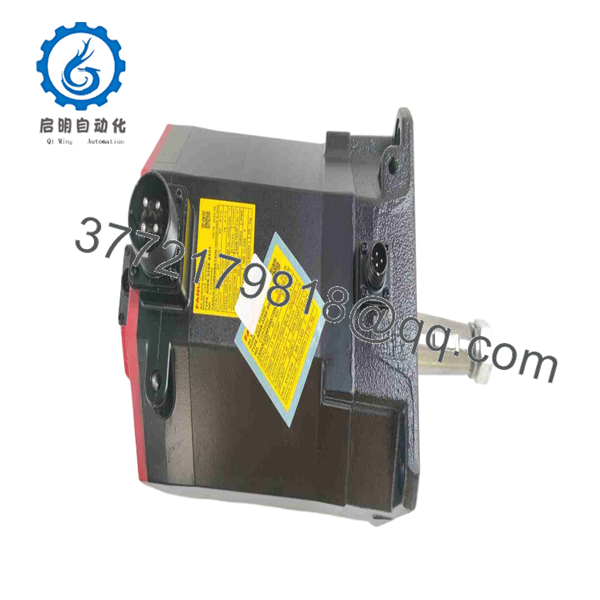
A06B-0268-B605
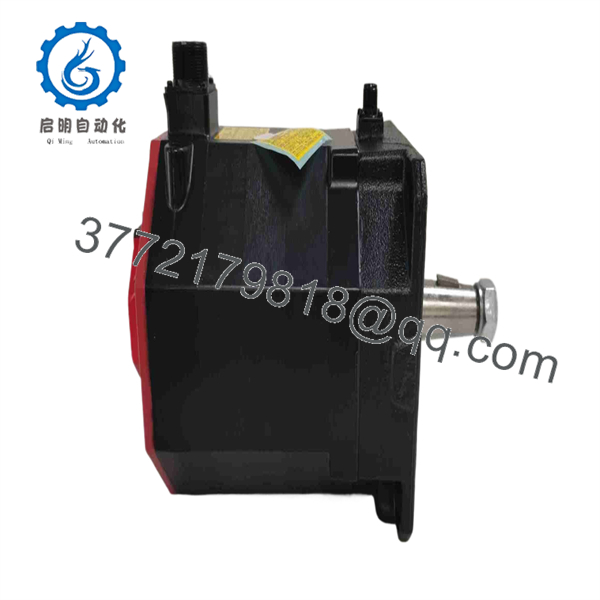
A06B-0268-B605
6. Frequently Asked Questions (FAQ)
Q: Is this motor a direct replacement for other AiS30/4000 variants?
A: It matches the AiS30/4000 electrical and mechanical footprint with tapered shaft and 90 V brake. Confirm the exact encoder type (a64ia) and amplifier model. Shaft keyway or flange details can differ slightly between suffixes—measure the old unit or check the drawing before ordering.
Q: What condition is this unit and why is the price lower than factory new?
A: This is New Original / New Surplus stock. It has never been installed in a machine. Units are inspected, functionally tested under load on a compatible Alpha i amplifier, and shipped with a 1-year warranty. Factory lead times and list pricing are higher; surplus inventory fills the gap for urgent replacements.
Q: Can I hot-swap this motor?
A: No. Always power down the servo amplifier and release residual energy before disconnecting power or encoder cables. Hot-swapping risks damaging the amplifier power stage or encoder electronics.
Q: Does the motor retain absolute position after power loss?
A: Yes. The a64ia absolute encoder holds position data. After power restoration the CNC can recover position without a reference return, provided the battery or absolute data backup on the control side is intact.
Q: What amplifier does this motor require?
A: It pairs with FANUC Alpha i series servo amplifiers sized for the 30 Nm / 5.5 kW rating. Confirm the amplifier current capacity and parameter set match the motor. Using an undersized amp will cause overcurrent alarms under load.
Q: What are the most common installation mistakes?
A: Failing to release the 90 V brake before rotating the shaft by hand, mixing up encoder cable pinouts, and skipping the motor ID / parameter check in the CNC. Take a clear photo of the old motor’s connectors and nameplate before removal. Mirror the wiring exactly and verify parameters before the first power-up.
Q: Is firmware or parameter backup needed when replacing?
A: The motor itself has no user firmware. All tuning lives in the CNC and amplifier. Back up the current parameter set and note the old motor ID before swap. After installation, confirm the new motor ID is recognized and run a basic axis test at reduced speed.